
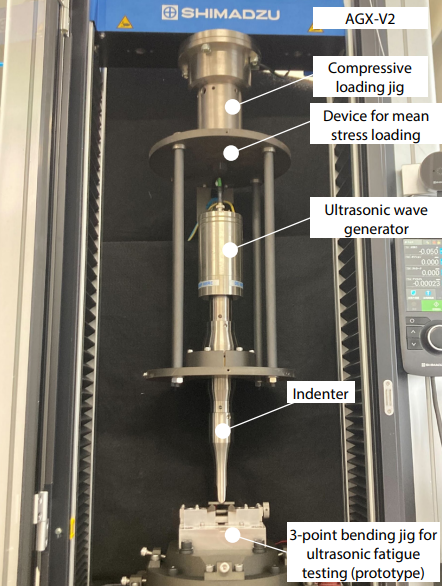
Carbon fiber reinforced plastic ultrasonic fatigue testing utilizes the Shimadzu USF-2000A system at a 20 kHz frequency to compress a $10^9$ cycle durability assessment from months down to roughly 14 hours.
Ultrasonic Frequency Loading Configurations
Assessing fatigue in carbon fiber reinforced plastic (CFRP) remains vital for durability across sectors like transportation, aerospace, automotive, shipbuilding, and civil engineering, where materials undergo intense cyclic loads. Traditional fatigue testing machines require several months to complete a $10^9$ cycle test. To bypass this bottleneck, the Shimadzu USF-2000A ultrasonic fatigue testing system operates at a 20 kHz frequency. This ultrasonic oscillation allows engineers to finish a billion-cycle test in approximately 14 hours.
ScienceDirect noted that CFRP laminates exhibit superior specific strength, specific gravity, and corrosion resistance compared to traditional metals. However, the fatigue damage mechanism of fiber-reinforced polymer laminates involves interacting phenomena such as matrix cracking, matrix-fiber debonding, delamination, and fiber fracture. These factors accumulate and degrade mechanical properties like stiffness and strength until final breakage occurs. Traditional models like S-N curves and Goodman fatigue life curves lack adequate consideration for these complex damage coupling mechanisms without substantial empirical data. To account for composite property degradation under fatigue, investigators have proposed numerous residual stiffness and residual strength models. Notably, the model formulated by Shokrieh and Lessard incorporated laminate anisotropy and interactions between damage modes, yielding more accurate predictions of damage evolution, residual stiffness, and residual strength under fatigue loading, while reducing dependence on experimental data.
For the experimental setup on the USF-2000A, researchers prepared a CFRP specimen measuring 40 mm in length, 7 mm in width, and 3.5 mm in thickness. Because ultrasonic fatigue testing requires resonance of the test sample at 20 kHz, setting an exact span is critical. The test configuration utilized a span of 16.5 mm alongside a three-point bending indenter and a prototype jig derived from the system’s average stress loading mechanism. Instrument configurations span a Shimadzu USF-2000A ultrasonic fatigue testing system, an AGX-V2 precision universal testing machine, test jigs incorporating a device for mean stress loading, a compressive loading jig, an R5 indenter, and a three-point bending jig utilizing support R2, all operated via Super Sonic software.
High-Speed Video Recording and Digital Image Correlation Analysis
Observing high-frequency specimen behavior requires specialized optical equipment. An HPV-X2 high-speed video camera captured the sample behavior during testing at a frame rate of 1 Mfps. Before recording, researchers applied a random pattern for Digital Image Correlation (DIC) analysis directly onto the specimen.
The resulting DIC analysis tracked displacement in the test axial direction directly below the ultrasonic indenter. The resulting sine wave confirmed that the loading mechanism performed properly during high-frequency oscillation.
Comparative Fatigue Performance and Thermal Management
During the three-point bending ultrasonic fatigue test, managing heat build-up is essential. The testing protocol incorporated an air cooler along with interval operation, turning oscillation on and off in cycles. A KEYENCE FT-H10 radiation thermometer monitored the surface temperature of the test samples continuously. Static three-point bending tests established a maximum test force of 3479 N, with results detailed in a force-strain diagram.
The applied test force during ultrasonic cycling was set between 65% and 85% of the peak test force established in the static bending test, operating at a stress ratio of 0.7 up to a maximum of $1.0 times 10^9$ cycles. Additional tests run on traditional fatigue testing machines under greater test forces yielded lower cycle counts before fracture.
While ultrasonic testing systems offer high-speed validation, non-destructive testing techniques remain necessary to evaluate internal conditions before catastrophic failure. Methods such as pulse-echo ultrasonic tests, infrared thermography, and X-ray computed tomography detect internal porosity and delamination. Fatigue damage naturally introduces internal porosity as cyclic loading expands micro-cracks. Ultrasonic evaluation methods provide high sensitivity to these structural defects, making them ideal for structural health monitoring in engineering environments. In evaluations of fatigue failure regions on CFRP bars using pulse-echo ultrasonic tests, A-scan echo signals clearly delineated the depth and area of internal delamination.
Field Inspection Protocols and Defect Localization
Onsite testing and defect documentation follow strict personnel and equipment requirements, including compliance with the PRE-PL-LO-004 Personal Health and Safety Plan and PRE-PL-LO-005 Personnel Qualifications. Field equipment necessitates an ultrasonic testing system, wire brush or hand broom, tape measure, temporary marker, digital camera, and a clipboard with pencil and sketch pad.

Defect localization utilizes a segmentation and numbering system known as the Structure Segmentation and Element Identification System (FLD-OP-SC-002) to assign a unique element identifier. Technicians employ the Determination of Local Origins for Elements procedure (FLD-OP-SC-003) to establish a local origin on each element, identifying relevant coordinate axes such as x and z for a girder web. Surface preparation requires cleaning suspect bridge elements with a wire brush, followed by manufacturer-calibrated system testing. During testing, transducers are configured to detect voids larger than half the wavelength, utilizing wedges and couplant to propagate waves, determine material thickness, record reflected waves, convert waveforms into frequency spectra, and determine distances to identified defects. Upon flaw detection, operators scan the area, estimate crack length from beginning to end using the ultrasonic system and tape measure, and mark these points. Final crack documentation records the unique superstructure element identifier, logs the beginning and ending points using y, z coordinates, describes the precise location relative to structural connections, and records crack length in decimal inches alongside maximum crack width measured with a crack comparison card or crack gage.
